
By FencingWise Editorial Team · Updated 17 September 2026.
Start with stable item codes and the assemblies those items support.
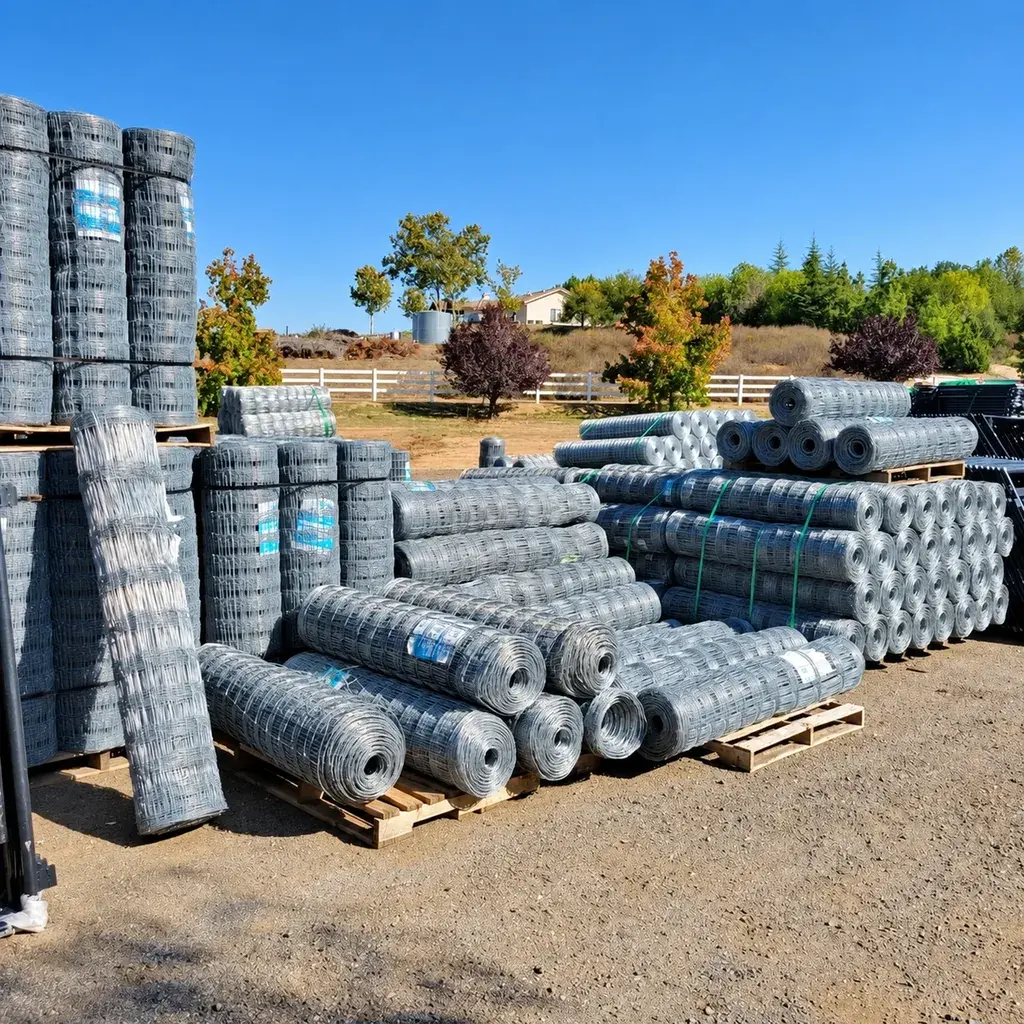
Separate regular demand from exceptional projects
Repeated distributor sales can be planned using recorded demand and replenishment experience. A one-off project with unusual heights, colours or gates needs a separate allocation; treating it as normal monthly demand can distort the next purchase.
Review demand by compatible item or family. Two similarly named panels may use different clips or post arrangements. Combining their sales can produce a reasonable total and the wrong mix.
Use the importer specification-sheet method to retain dimensions, connections, finish and revision alongside each stock code.
Calculate a simple reorder point
A basic planning model is:
Reorder point = expected demand during replenishment lead time + chosen safety stock.
Assume a fictional standard panel sells at 50 units per month, with a replenishment lead time of 2 months and a deliberately selected buffer of 25 units.
Expected demand during that lead time is 50 × 2 = 100 units. The reorder point is:
100 + 25 = 125 units.
The buffer of 25 is an assumption, not an industry recommendation or a statistically calculated service level. Actual demand variability, lead-time variation, order frequency and the cost of shortages should inform the chosen method.
This model is useful when its assumptions are visible. It should not be presented as a guarantee that stock will never run out.
Compare the reorder point with stock position
Physical stock alone can be misleading. A simple inventory-position calculation is:
On hand + confirmed incoming − committed demand.
Suppose the fictional distributor has 80 panels on hand, 60 confirmed incoming and 40 already committed to orders. Its position is:
80 + 60 − 40 = 100 panels.
That is below the 125-unit reorder point. If the chosen order-up-to position is 200 units, the preliminary replenishment quantity is:
200 − 100 = 100 panels.
The 200-unit target is another explicit planning assumption. Check supplier pack sizes, minimum order arrangements, storage space and cash commitments before finalising the purchase.
Check arrival dates, not only the total
The inventory-position calculation can conceal a timing gap. Incoming panels due after a committed delivery date cannot fulfil that earlier order.
Maintain a dated projection where timing matters: opening usable stock, expected receipts, committed dispatches and closing usable stock for each period. Keep uncertain receipts distinguishable from confirmed ones.
For example, 60 incoming panels do not help a dispatch tomorrow if they are due next month. That order must be assessed against currently available, compatible stock and any reliable earlier receipt.
The lead-time scheduling method explains why production completion and arrival are separate milestones.
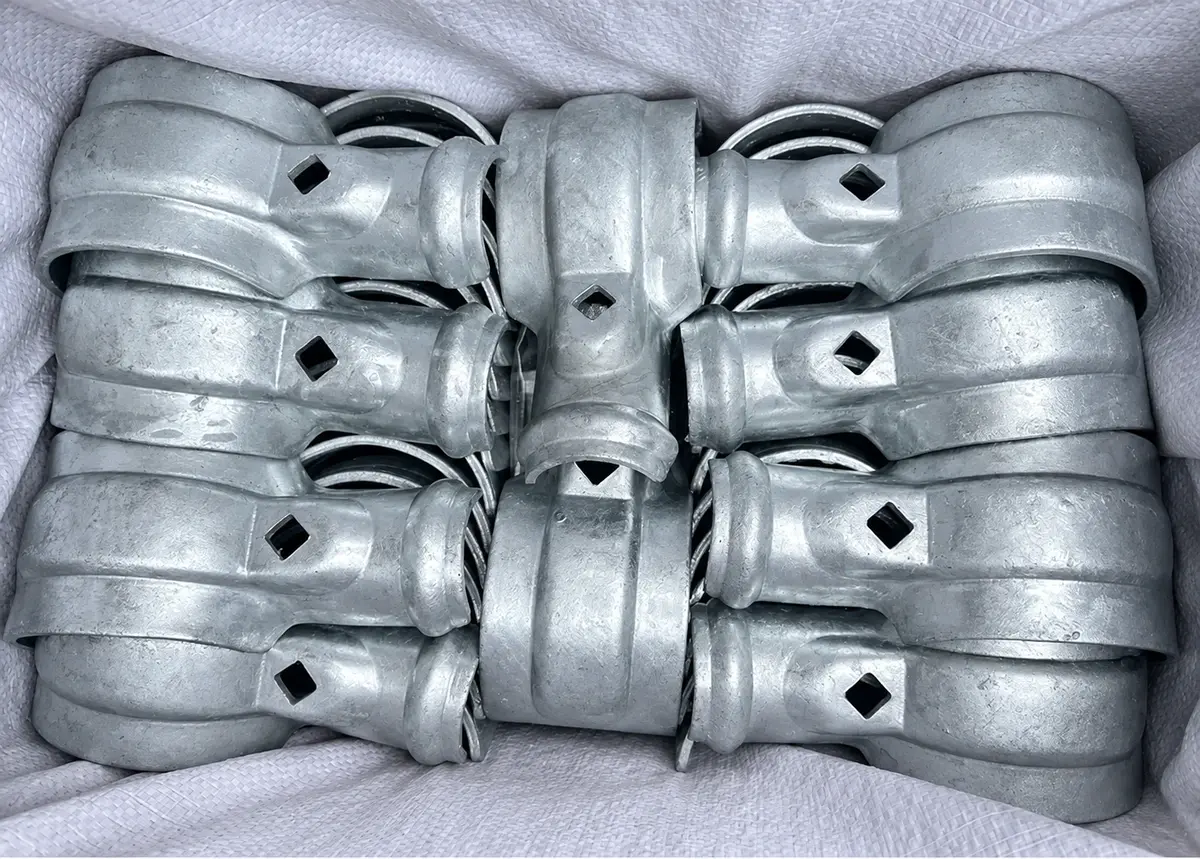
Plan components in complete assembly ratios
Assume a hypothetical panel requires 8 independent complete fixing sets under its approved connection detail. Supporting 50 panel sales requires 50 × 8 = 400 sets, before the chosen spare or service allowance.
If a set contains one clamp, one bolt, one nut and two washers, 400 sets need 800 washers. A stock record with 400 clamps but only 600 washers can form only 300 complete sets, assuming all other parts are available.
That supports 300 ÷ 8 = 37 complete panel fitting allocations, with four sets left over. The warehouse's clamp count alone would overstate the number of fully supported panel orders.
The eight-set assumption belongs to this example. Derive the ratio for each actual connection and do not apply it to shared-clip or clamp-bar systems.
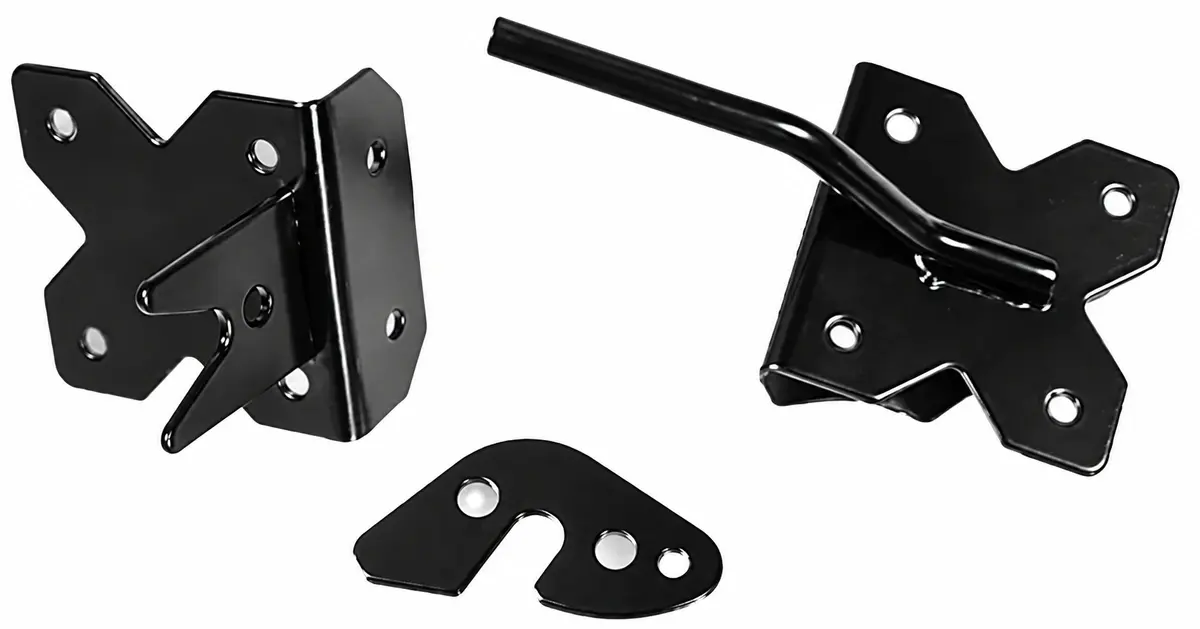
Keep repair kits separate from ordinary bulk parts
A useful repair kit contains the compatible panel or hardware and the parts needed to complete that repair. Permanent fasteners, unusual bracket lengths or proprietary caps can determine whether the kit is usable.
Classify stock by consequence as well as sales volume. A low-volume gate receiver might be important because its absence prevents an entrance from operating. A commonly sold standard cap may be easier to replenish locally.
This is not a reason to stock every possible part. Use the installed base, failure or replacement history, availability and substitution options to decide which low-volume items merit holding.
Control revisions and mixed batches
When a specification changes, determine whether existing and new stock remain interchangeable. A matching external size does not prove compatibility if internal openings, fixing positions or coating requirements changed.
Label incompatible revisions separately. Record which version belongs to each retained repair kit or project allocation. If a part is superseded, define whether it can still support older installations or should be withdrawn from general picking.
Appearance can also matter. Components from different coating batches may meet the agreed specification yet need a planned visual comparison for side-by-side use. Retain batch identity rather than losing it during warehouse consolidation.
Review the plan against actual results
Track stockouts, emergency purchases, slow-moving items, unusable mixed sets and demand that was incorrectly forecast. Distinguish ordinary sales from exceptional projects.
Then update the demand and lead-time assumptions at a suitable review interval. If the example's lead time rises from two to three months while demand and buffer remain unchanged, its reorder point becomes 50 × 3 + 25 = 175 units, an increase of 50.
Do not change every buffer automatically after one unusual event. Identify whether the cause was demand, supplier timing, a revision error or incomplete component kits.
A workable stock plan ends with available assemblies, clear allocations and a traceable replenishment decision. That supports B2B customers more reliably than a warehouse full of panels whose matching parts have run out.